Sealless Pumps for a Safer and Greener World

Choosing a weld fixture manufacturer in China involves more than comparing prices or browsing product photos. Weld Fixture Tooling must hold parts in the correct position, support repeatable welds, and allow practical access for operators or automated equipment. A fixture that looks precise on a drawing may still create problems on the shop floor. Small details matter.
This guide introduces manufacturers and explains what buyers can examine before requesting a quote. Look for evidence of experience with your part type, material, production volume, and welding process. Ask how the supplier handles design reviews, clamping access, locating accuracy, and expected weld distortion. Clear drawings, inspection records, and realistic delivery schedules can help reveal how a company works. They are not guarantees, though.
A useful supplier should be willing to discuss trade-offs, not simply promise perfect results. For example, a lighter fixture may be easier to handle but less stable under repeated use. Requesting sample project details or a proposed inspection plan can make comparisons more meaningful. Communication matters, especially when specifications change or a trial exposes a problem. This is where experience shows.
The manufacturers covered here should be assessed against your own requirements, not treated as a universal ranking. Supplier capabilities vary, and public information may not tell the whole story. Verify important claims directly, clarify responsibilities, and consider a production trial when practical. A careful choice can reduce rework and support consistent welding, but no supplier can remove every manufacturing risk.
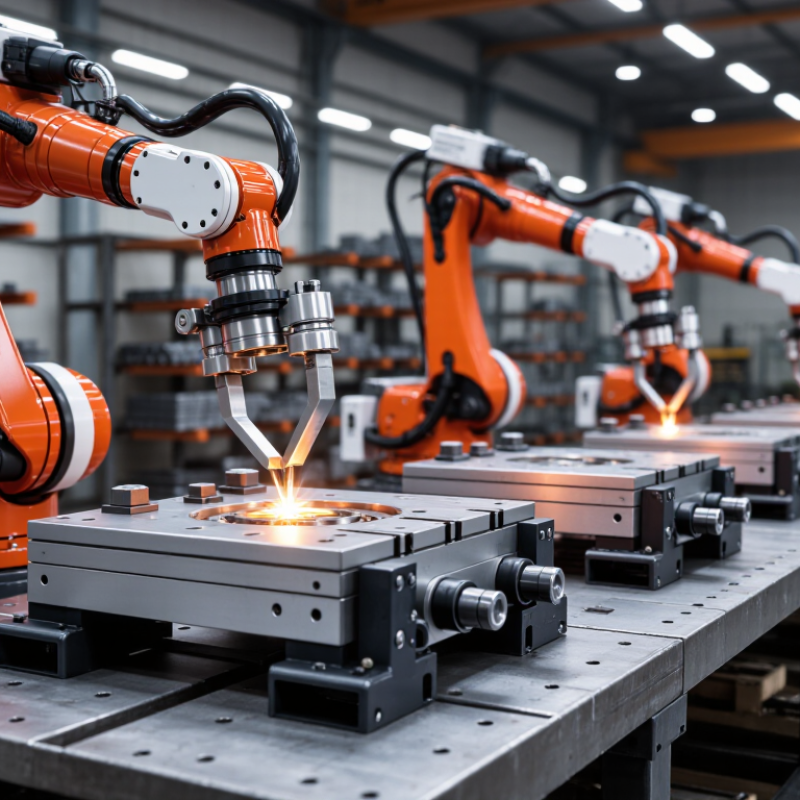
A weld fixture is a purpose-built device that holds metal parts in position during welding. Its stops, pins, clamps, and locating surfaces help control alignment before heat changes the material. On a production floor, even a small shift can leave a bracket tilted or a gap uneven. The fixture gives operators a repeatable starting point. It is not magic.
Good tooling supports both accuracy and practical workflow. A clamp should secure the part without blocking the welding torch or forcing awkward hand positions. Locators need to reference surfaces that remain consistent from one workpiece to the next. Designers also consider weld access, part removal, and heat distortion. These details matter when a component must fit against another assembly later.
Fixture performance depends on use and upkeep, too. Spatter can build up around contact points, while worn pins may gradually affect alignment. Regular checks with a simple gauge can reveal drift before it creates a batch of poor-fitting parts. Still, a fixture cannot correct every upstream variation. That limitation is easy to overlook. Reviewing actual parts with operators often exposes problems that drawings alone miss. A well-designed weld fixture makes a process more stable, but its value depends on thoughtful setup, inspection, and feedback from the people using it.
How to Evaluate Weld Fixture Tooling Manufacturers in China
Evaluate engineering evidence, not showroom polish. Ask for fixture drawings showing datum strategy, clamp locations, weld-gun access, and service points. A useful review also checks whether the supplier can explain how parts are located and how distortion is managed. No checklist catches everything. Request a trial build using representative parts, then measure repeatability across several loading cycles. Record gaps, clamp marks, and access issues; these details can reveal problems that a presentation will not.
Production context matters. The International Federation of Robotics’ World Robotics 2024 report recorded 276,288 industrial robot installations in China during 2023, about 51% of worldwide installations. That scale makes automation compatibility worth checking, but it does not prove a fixture supplier’s quality. Ask for interface details, sensor provisions, and documented revision control. Also examine machining inspection records, material traceability, and the supplier’s response process when a design changes. Evidence should be specific.
Talk with the engineers who will handle commissioning, not only sales staff. Ask how they verify clamp force and protect access for maintenance. A capable team should explain trade-offs plainly, including limits. If the first trial is imperfect, that is not automatically a red flag; vague corrective actions are. Request a dated action list and retest criteria before accepting the fixture.
| Evaluation dimension | What to verify | Useful evidence or acceptance basis | Suggested weight | Score (1–5) |
|---|---|---|---|---|
| Engineering and fixture design | Ability to interpret part data, welding sequence, datum strategy, clamp access, and process requirements. | Review a design proposal, 3D model, clamp layout, and documented design-review process against your part and weld-process requirements. | 20% | _____ |
| Accuracy and repeatability | How fixture locating features and assembled components are measured and checked for repeatable part positioning. | Request inspection records for critical dimensions and a measurement plan. Agree tolerances from the part drawing and application; avoid relying on a generic accuracy claim. | 15% | _____ |
| Manufacturing capability | In-house or controlled capability for machining, fabrication, assembly, and any required surface treatment. | Check relevant equipment, process controls, subcontracting arrangements, and sample inspection documents for comparable work. | 15% | _____ |
| Welding-process understanding | Consideration of weld access, torch or gun clearance, heat distortion, spatter, and operator or robot access. | Review process-specific layout checks and a trial or simulation plan where appropriate. Confirm compatibility with the customer’s welding process and equipment. | 15% | _____ |
| Materials and purchased components | Suitability and traceability of specified steels, aluminum, locating elements, clamps, sensors, and other components. | Confirm the bill of materials, material certificates where specified, component datasheets, and an approval process for substitutions. | 10% | _____ |
| Quality management and documentation | Document control, inspection records, nonconformance handling, and change management throughout the project. | Review sample quality records and audit relevant certifications directly with the issuing body. ISO 9001 certification can support assessment of a quality-management system but does not certify fixture performance. | 10% | _____ |
| Project delivery and communication | Realistic milestones, drawing-approval points, progress reporting, and responsiveness to technical questions. | Request a project schedule showing design, approval, fabrication, inspection, tryout, and shipment stages; check how delays and design changes are communicated. | 10% | _____ |
| Tryout, installation, and after-sales support | Support for fixture validation, installation, operator handover, spare parts, and issue resolution after delivery. | Define acceptance tests, included support, response channels, spare-parts arrangements, and any travel or service costs in the quotation or contract. | 5% | _____ |
| Total suggested weighting | 100% | _____ | ||
Scoring guide: 1 = insufficient evidence; 3 = meets agreed requirements; 5 = strong, documented evidence. Compare weighted scores only after confirming that each supplier has quoted the same scope, specifications, and acceptance criteria.
China’s weld fixture tooling sector benefits from a large, automation-focused manufacturing base. The International Federation of Robotics reported 276,288 industrial robot installations in China in 2023, about 51% of global installations. This figure signals strong demand for integrated production systems, but it does not measure fixture quality directly.
Capable manufacturers typically demonstrate repeatable locating accuracy, stable clamping, and practical maintenance access. During evaluation, inspect machined datum surfaces, clamp reach, sensor placement, and access for weld-gun servicing. Ask for dimensional inspection records and trial-run results from comparable assemblies. A fixture can look precise on a drawing and still cause rework.
Details matter. A lot.
Production teams should also assess how suppliers manage design changes, spare components, and communication between tooling and automation engineers. IFR’s data is useful context, not a supplier ranking. Buyers should verify capacity and performance through audits and part trials. I would not treat a polished sample fixture as proof of long-term consistency; that judgment needs production evidence.
Comparing Chinese weld-fixture manufacturers means looking beyond quoted price. A capable supplier should show experience with datum planning, clamp access, weld sequence, and repeatable part location. In 2023, China installed 276,288 industrial robots, 51% of global installations, according to the International Federation of Robotics’ World Robotics 2024 report. This signals a large automation ecosystem, but does not prove any individual tooling supplier’s quality. Ask for measured tryout results, tolerance records, and examples of fixtures built for similar materials and part sizes. Small details matter.
Product range is another useful comparison. Some manufacturers focus on manual fixtures and checking gauges; others integrate robotic welding cells, safety guarding, and offline simulation. Check whether their design includes clear sensor access, replaceable locators, and room for operators to load parts without awkward reaches. A polished CAD model can still hide a poor clamp position. Not always obvious. Service matters after delivery, too: clarify who handles installation, run-off, spare components, and revisions when production changes. Factory visits and documented acceptance checks provide stronger evidence than catalogue claims, though they take time and may not reveal every weakness. A supplier’s response to a failed trial can be as revealing as its initial quotation.
When sourcing weld fixture tooling from China, judge the supplier’s process, not just the quoted price. Request a layout drawing, datum strategy, material specifications, and a written inspection plan before approving production. Ask how the team controls clamp position, weld access, and distortion after repeated heat cycles. These details affect whether parts locate consistently on the shop floor.
China’s manufacturing scale can support complex projects, but scale alone does not guarantee fixture quality. The International Federation of Robotics reported 276,288 industrial robot installations in China in 2023, representing 51% of global installations. This reflects a substantial automation ecosystem, not proof that any individual tooling supplier meets your requirements. Review sample inspection records and observe a tryout using actual parts. A clean demonstration video is not enough. I would still allow time for one design adjustment; real parts can expose issues that CAD misses.
Tips: Put acceptance criteria in the purchase order. Specify critical dimensions, repeatability checks, spare locating pins, and the format for inspection reports. Confirm packaging, export documents, and delivery milestones early. Keep a signed drawing revision on file. Small changes can otherwise become expensive surprises.