Sealless Pumps for a Safer and Greener World

Choosing the right Defect Marking System starts with understanding the defect, the product, and the production line. A mark must remain visible on the actual surface, whether it is brushed metal, molded plastic, or a moving carton. It also needs to identify the fault without confusing operators or disrupting throughput. Small details matter.
W. Edwards Deming, a widely recognized quality-management expert, wrote, “Quality comes not from inspection, but from improvement of the production process.” That principle helps frame this decision: marking should support timely action, not merely label a problem after it occurs. A system’s value depends on how clearly its marks guide inspection, rework, or removal. This is where real-world trials matter. Test the ink, laser, or label against surface finish, line speed, cleaning routines, and the conditions where products are stored. A mark that looks crisp in a sample room may fade under oil, heat, or handling.
The outline that follows compares marking methods, integration needs, readability, operating costs, and maintenance demands. It also considers how operators will apply and verify each mark during a busy shift. There is no perfect setup. A fast system may cost more to maintain, while a low-cost option may require frequent checks. That trade-off is easy to underestimate. Use measurable criteria, involve the people who will run the equipment, and confirm results on production samples before committing. A careful choice makes defect identification clearer and helps keep the process consistent.
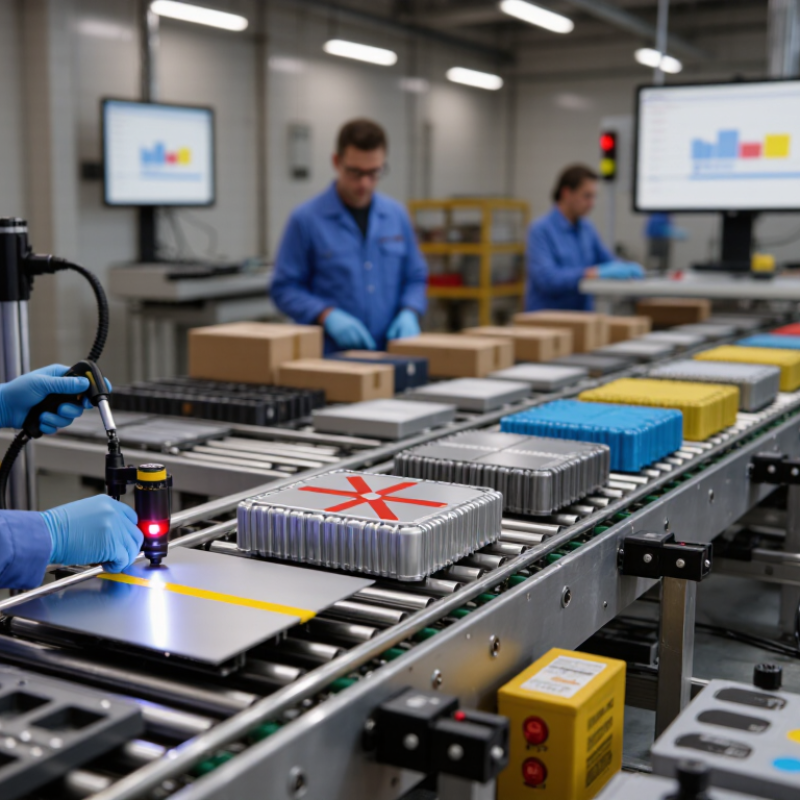
A defect marking system makes nonconforming parts easy to identify, separate, and review. Its purpose is practical: prevent a flawed item from moving unnoticed to the next operation. Manual paint pens or tags suit low-volume work, where an operator can inspect each piece. Inkjet systems apply quick, visible codes on moving production lines. Laser marking creates durable marks, but material compatibility and surface appearance need testing. Vision-guided systems can detect defects and trigger a mark automatically. Different needs, different tools.
Tips: Test marks on real parts, not just sample cards. Check readability after handling, cleaning, or heat exposure. A mark that fades is a weak signal.
Choose based on defect type, line speed, surface, and what happens after marking. A temporary color may be enough for parts awaiting inspection; traceable codes may help when teams need to track rework or recurring faults. Confirm that operators can distinguish defect categories under actual lighting. Also consider whether the system records who marked the item and when. Automation can reduce missed marks, but it still needs calibration and routine checks. It is tempting to choose the fastest option. Yet a slower, clearer mark may prevent confusion downstream.
Before comparing a defect marking system, define what each mark must communicate. A scratch, dent, missing component, and contamination issue should not share an ambiguous code. Build categories around observable conditions, not vague labels such as “bad part.” For each category, record severity, location, disposition, and inspection evidence. A hairline crack near a mounting hole may need a different response from a shallow surface scuff. Keep category names short enough for operators to use consistently. Test them on real samples. Some edge cases will still resist neat classification.
Then specify marking requirements at the point of use. Decide whether marks must survive handling, washing, heat, or later processing. Set rules for size, color, placement, and legibility, including limits near functional surfaces. A red dot can be quick, but it may disappear under oil or become hard to see in dim lighting. Define who applies the mark, who verifies it, and how the code links to the inspection record. Capture a photo when location or shape matters. Keep a simple reference card beside the station. Keep it visible. Recheck it when products or workflows change. In practice, people may improvise if instructions are hard to follow. That risk is worth acknowledging.
How to Choose the Right Defect Marking System?
Laser, inkjet, dot peen, and labels each suit different production needs. Laser marking can create durable, high-contrast codes, but results vary with wavelength, coating, and material. Inkjet handles changing messages quickly; ink must match the surface and operating conditions. Dot peen forms tactile marks on many metals, though noise and surface deformation may matter. Labels offer flexibility, but edges can lift in heat, oil, or cleaning.
MarketsandMarkets estimated the global laser marking market at about $3.2 billion in 2023, projecting $4.5 billion by 2028. This signals growing industrial adoption, not that laser is best for every line. Test actual parts: a dark mark on brushed steel may disappear under glare, while a plastic housing may warp under excess heat. Check readability, abrasion resistance, cycle time, and inspection-camera performance. One trial is not enough.
Tips: Test on production-grade samples, including coatings and surface finishes. Compare marks after handling and cleaning. Record contrast and reject rates. There is no flawless winner; pilot tests can still miss shifts in material batches or line speed. Use results from repeated runs before choosing a method.
| Technology / Method | How It Marks | Suitable Materials | Mark Characteristics | Production Fit | Key Advantages | Limitations and Checks |
|---|---|---|---|---|---|---|
| Continuous inkjet (CIJ) | Projects small droplets of liquid ink onto a surface without requiring the part to stop. | Many non-porous surfaces, including metals, plastics, glass, and coated materials; ink must be matched to the substrate. | Typically a small, fast-drying text, code, or spot. Durability depends on ink chemistry, surface condition, and exposure. | High-speed lines and moving products; can be integrated with sensors or inspection equipment. | Non-contact marking; supports rapid marking and variable information. | Requires ink and solvent management. Verify adhesion, drying time, contrast, and resistance to oils, abrasion, or cleaning chemicals. |
| Thermal inkjet (TIJ) | Heats ink in a cartridge to form droplets that are deposited on the product. | Paper, cardboard, and selected plastics, metals, or coated surfaces when compatible ink is used. | Sharp characters and codes; permanence varies with ink formulation and substrate. | Intermittent or moderate-speed marking, especially where clean, compact equipment is useful. | Non-contact process; cartridge-based ink supply can simplify routine replacement. | Cartridges require replacement, and print performance can depend on distance, surface texture, and environmental conditions. |
| Laser marking | Uses a focused laser to change a surface by discoloration, engraving, foaming, or material removal, depending on the material and process. | Metals and selected plastics, ceramics, glass, or coatings; the appropriate laser and settings depend on the material. | Can create durable marks without ink. Mark appearance and depth vary by material and process. | Automated production cells and applications needing repeatable, permanent marks. | No ink or label consumables; precise, programmable marking. | Higher initial system and integration requirements. Assess laser safety, extraction needs, heat effects, and whether the mark changes material properties. |
| Dot peen (impact marking) | A carbide or hardened stylus makes a pattern of small impact points on the surface. | Metals and other sufficiently rigid materials; suitability depends on hardness, thickness, and part support. | Permanent indented characters, codes, or patterns; the mark is physically formed in the surface. | Stationary parts or controlled fixtures; commonly used where a durable identification mark is needed. | Does not rely on ink or surface color; marks can remain visible after some surface treatments. | Creates noise and surface deformation. Consider part vibration, thin-wall damage, cosmetic requirements, and whether the indent could affect function. |
| Scribe marking | A hard point is drawn across the surface to create a continuous groove. | Primarily metals and other materials that can be scratched consistently. | Continuous, permanent line or character marks; visibility depends on lighting, finish, and groove depth. | Controlled, usually stationary marking of rigid components. | Can produce clear, durable marks with less impact vibration than dot peen. | Leaves a groove and may affect coatings or corrosion protection. Test mark depth, surface finish, and downstream cleaning or finishing requirements. |
| Paint or industrial marker | An operator or automated applicator deposits a visible line, dot, or symbol using paint or marker ink. | Many surfaces, including metal, wood, concrete, and some plastics; formulation must suit the surface and environment. | Highly visible temporary or semi-permanent mark; removal and wear resistance vary by product. | Manual sorting, rework areas, and low-volume or flexible workflows. | Simple to deploy; useful for large, conspicuous visual marks and irregular locations. | Consistency can vary with operator and application. Check drying, smearing, chemical compatibility, and whether the mark is acceptable on the finished product. |
| Adhesive label or tag | A printed label or tag is attached to the part, package, or container. | Flat or suitably shaped surfaces that provide adequate adhesion; label stock and adhesive must match the substrate and conditions. | Can carry text, barcodes, or other identification; may be removable or permanent depending on label construction. | Manual or automated application; useful when information needs to be readable without altering the product surface. | Supports detailed information and can avoid direct marking of sensitive surfaces. | Labels may peel, become obscured, or be damaged by heat, moisture, chemicals, or abrasion. Validate adhesion and traceability throughout handling. |
Selection tip: First define the required visibility, permanence, mark size, line speed, substrate, and downstream handling. Trial the chosen method on representative parts under actual production and cleaning conditions before implementation.
A marking system must fit the production line, not just the defect list. Check how it connects with existing sensors, cameras, and control software. Can it receive a reliable defect signal and mark the correct item without slowing the line? Test this with real products, including awkward shapes and changing orientations. Small integration gaps matter. A missed trigger can send good parts to rework.
Safety needs practical checks at the workstation. Look at guarding, access for maintenance, and the handling of inks or other marking materials. Operators should be able to clear a jam without reaching near moving equipment. Ask how the system behaves after a fault or power interruption. The safe setting on paper may feel cumbersome during a busy shift; that deserves attention, not dismissal.
Measure speed under normal operating conditions, not only at the machine’s advertised maximum. Track marked items per minute, setup time, and delays caused by cleaning or replenishment. Then estimate operating costs across a typical month: consumables, energy, maintenance, rejected parts, and downtime. A low purchase price can hide frequent service needs. Keep the figures visible. A short production trial, with operators recording stoppages and mark quality, can expose assumptions that a spreadsheet misses. Some results will be messy. That is useful.
How to Choose the Right Defect Marking System?
A defect marking system should fit the way your line actually runs, not just look impressive in a demonstration. Test it on your own parts, materials, and line speed. Mark a dull metal surface, a glossy plastic edge, and a part with light oil residue. Check whether marks remain readable after handling, cleaning, and downstream processing. ASQ’s quality-cost guidance notes that poor quality can cost organizations up to 15% of sales, making dependable defect identification more than a cosmetic choice. Treat that figure as a warning, not a prediction for every plant.
Tips: Run a short trial during a normal production shift. Track missed marks, false rejects, changeover time, and operator adjustments. Ask operators to use the system without extra coaching. Their workarounds matter. So do small failures. A mark that looks clear under inspection lighting may disappear beside a conveyor’s shadow. Record results by part type and shift, then compare them with your current process. Don’t assume the fastest setup will be the most reliable.
Also test how the system handles recipe changes and maintenance. A practical choice should make settings easy to verify and recovery steps easy to follow. Keep the trial imperfect on purpose: include a rushed changeover or a dusty part, then note what failed. Your real workflow is rarely as tidy as a lab bench.
Compare marking options against the needs of your production workflow. The example scores below use a 1–5 scale, where 5 is best; they are illustrative pilot-test results, not universal performance ratings.